

Torch Height Control helps maintain the correct torch-to-sheet distance during CNC plasma cutting, supporting consistent edges and longer consumable life. Learn how THC differs from IHS, what happens when the torch is too high or low, and how to manage piercing, corners and small holes.
CNC plasma cutting enables fast production of parts from structural steel, stainless steel and aluminium. Cutting current, travel speed, gas quality and consumables influence the finished edge. Equally important is the distance between the torch and sheet. THC automatically adjusts this height during cutting to compensate for uneven material.
Correctly configured Torch Height Control supports repeatability, but cannot replace suitable cutting charts, surface sensing or CAM programming. Explore CORMAK plasma cutting machines for examples of available equipment.
What is THC in a CNC plasma cutter?
THC stands for Torch Height Control and manages the Z-axis while cutting. Many systems monitor arc voltage. Changes in arc length affect voltage, so the controller can raise or lower the torch to maintain the required distance.
Not all systems use identical measurement methods or control algorithms. Response speed, delays, anti-dive behaviour and handling of changes in travel speed depend on the plasma source, CNC controller and Z-axis mechanics. Settings must follow the relevant cutting charts.
THC and IHS perform different functions
IHS means Initial Height Sensing. Before piercing, it finds the sheet surface using a method such as ohmic or mechanical sensing. The controller then establishes a reference position, raises the torch to pierce height and subsequently moves to cutting height.
THC adjusts height during the relevant cutting phase. Pierce height, cut height and travel height are separate settings. They depend not only on thickness but also on current, gas, torch design and consumables.
Why does torch height affect cut quality?
The torch-to-work distance changes arc geometry, kerf width, edge bevel, dross formation and piercing stability. Correct height helps maintain part dimensions when suitable kerf compensation is applied, and reduces the chance of contacting warped sheets.
- More consistent kerf width and edge finish.
- Better control of bevel, dross and small holes.
- Reduced likelihood of torch collisions.
- More predictable nozzle, electrode and shield wear.
THC cannot correct worn nozzles, incorrect speed, unsuitable gas or mechanical play. It is one element of the cutting process rather than a guarantee of square edges.
What happens when the torch is too high?
An excessive distance can reduce arc concentration, increase kerf width and positive bevel, and worsen dimensional accuracy. Small holes may be less accurate, and incomplete cuts can occur if the travel speed is also unsuitable.
These symptoms do not automatically prove a THC problem. Worn nozzles, incorrect current, gas pressure and travel speed can produce similar results. Check the full set-up before changing height settings.
What happens when the torch is too low?
Too little clearance increases the risk of hitting a warped sheet or previously cut parts. The shield, nozzle and electrode may be damaged or wear faster. During piercing, molten metal and spatter can strike the torch components.
Possible consequences include an unstable arc, burn marks, dross and downtime for replacement parts. Use the specified heights and review them after changing materials, current or consumables.
How does THC work step by step?
- Initial sensing: IHS finds the sheet surface and Z reference.
- Pierce height: the torch rises before arc initiation.
- Piercing: the controller observes the specified pierce delay.
- Cut height: the Z-axis adopts the required working distance.
- Height correction: THC reads the arc signal and adjusts Z.
- Travel: the torch rises before moving to the next pierce point.
The exact sequence and activation time vary by system. Arc voltage, height and delay settings must come from the manufacturer's data for the installed configuration.
Corners, small holes and piercing: when should THC be restricted?
The CNC slows down in sharp corners and small holes. This may alter arc voltage without any physical change in the sheet surface. Active THC can interpret the change as a height error and incorrectly lower the torch, a behaviour known as diving.
Depending on the controller, anti-dive, corner lock or temporarily freezing Z correction can prevent this. Piercing also requires a separate, usually greater, clearance to reduce the effect of molten-metal spatter.
How does THC affect quality and cutting costs?
Keeping the correct distance can reduce grinding, rework, collisions and premature consumable replacement. Benefits may be particularly useful for large sheets, thin material prone to warping and repetitive production. Compare the working areas of CORMAK plasma cutting systems.
Actual savings also depend on the cutting table, mechanical condition, CAM preparation, maintenance and cutting parameters. THC does not automatically guarantee dross-free results.
How to select and configure a THC system
Check compatibility between the plasma source, machine torch, arc-voltage interface, CNC controller and Z-axis drive. Consider the IHS method, smooth movement, anti-dive functions, CAM strategy and available cutting charts.
- Verify IHS, arc-voltage measurement and controller communication.
- Check Z-axis play and the condition of consumables.
- Set pierce, cut and travel heights separately.
- Configure corner-lock and small-hole strategies.
- Inspect the first part before starting a production run.
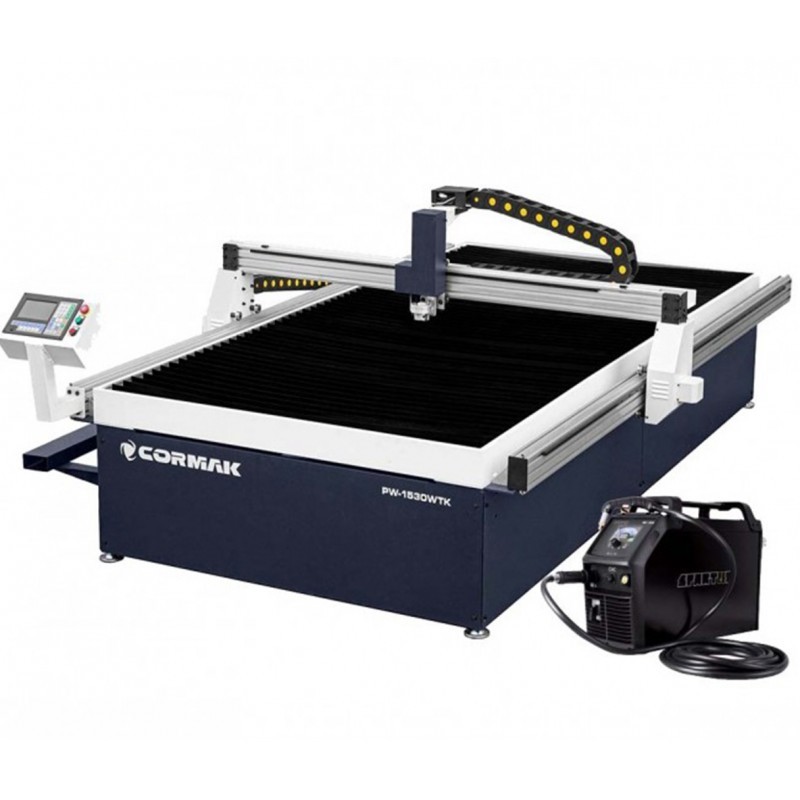
The Polish product listing describes the CORMAK PW-1530 WTK with ProCUT 125CNC with voltage-based THC and sheet detection. Confirm the exact specification before purchase.
Plasma cutting without and with active THC
| Area | Without THC | With correct THC |
|---|---|---|
| Warped sheet | Fixed Z position | Automatic clearance correction |
| Cut edge | Greater dependence on flatness | Potentially more consistent geometry |
| Consumables | Risk of incorrect clearance | Fewer unintended close approaches |
| Corners | Suitable CAM required | CAM and possible THC lockout required |
Working area and sheet support should also influence machine choice. The CORMAK PW-2040 WTK with water table is another model listed with THC in Poland.
Common signs of incorrect torch height
- Excessive dross, burrs or changing edge bevel.
- Wide kerf and inaccurate small holes.
- Piercing difficulties and rapid nozzle wear.
- Torch collisions with sheets or cut parts.
- Z-axis oscillation and diving in corners.
Before changing THC, inspect the work return connection, cables, electrodes, nozzles, gas, travel speed, mechanics and CAM. Electrical servicing must be performed by qualified personnel.
Frequently asked questions
Does every CNC plasma cutter need THC?
Not necessarily, but automatic height control is particularly useful for large or uneven sheets and repeat production.
Does THC detect the sheet surface?
Usually IHS detects the surface before piercing, while THC provides continuous adjustment during cutting.
Does THC improve small holes?
Correct height helps, but THC may need to be restricted when the machine slows and CAM strategies become more important.
Why does the torch dive in corners?
Reduced travel speed changes arc voltage, which may trigger an unnecessary Z correction. Anti-dive or corner lock can help.
Conclusion
THC helps maintain torch clearance and consistent cutting quality over uneven sheets. It must work alongside IHS, appropriate piercing heights, cutting charts, sound consumables and correct CAM programming.
Controlling gas, current, travel speed and mechanics while limiting inappropriate correction in corners can reduce rework, wear and unplanned downtime.
